Medovia Medical
High-precision monitoring sensors, sterilization systems, and diagnostic equipment engineered for worldwide clinical deployment.
A Whitepaper on High-Accuracy Sensor Technologies, Biocompatible Encapsulation, and China's Advanced Export Capabilities
In modern clinical diagnostics, critical care monitoring, and industrial thermal validation, precise thermal measurement is paramount. As a premier Top China Temperature Probes Supplier & Exporters, Jiangsu Medovia Medical Co., Ltd. leads the integration of advanced solid-state thermistors, platinum resistance thermometers (RTD Pt100/Pt1000), and custom OEM/ODM probe assemblies designed for rigorous global standards. Modern medical probes must maintain sub-fractional thermal resolution (down to ±0.05°C), rapid response time, biocompatibility, and immune response to electrosurgical interference (EMI).
Choosing the correct sensor element is vital for OEMs and international healthcare procurement agencies. Below is a comparative engineering overview utilized across our product line:
Primary Use: Patient Monitoring (Skin, Rectal, Esophageal probes).
Sensitivity: High (-3% to -5% R change per °C). Provides exceptional accuracy across human physiological ranges (32°C to 45°C).
Primary Use: Autoclave Sterilizers, Pharmaceutical Retorts, Laboratory Incubators.
Linearity: Excellent linear stability per IEC 60751 standard, capable of withstanding extreme thermal cycling (-200°C to +600°C).
Primary Use: High-temperature industrial heat treatment & HVAC ERV thermal recovery validation.
Response: Ultra-fast response times with high durability in hostile chemical environments.
Analyzing macro shifts toward micro-miniaturization, wireless telemetry, disposable hygiene protocols, and AI dynamic calibration.
Demands for minimally invasive catheters have pushed thermal probe OD sizes down to less than 0.5mm, requiring precision micro-soldering and laser welding.
Hospitals are shifting toward single-patient-use probes to eliminate Nosocomial infections (HAIs), accelerating high-volume precision manufacturing.
Continuous continuous body temperature tracking via wearable Bluetooth Low Energy (BLE) sensor patches integrated with central hospital monitoring networks.
Algorithmic drift correction on patient monitors compensates for ambient thermal gradients and contact resistance in real time.
Navigating vendor audits, biocompatibility standards, risk mitigation, and Total Cost of Ownership (TCO) optimization.
For international buyers, medical distributors, and hospital procurement officers, sourcing temperature probes and medical equipment from China requires rigorous supplier qualification. Sourcing managers evaluate suppliers across key criteria to ensure zero clinical failure rates:
Verification of ISO 13485 Quality Management Systems, CE Mark certificates under EU MDR 2017/745, FDA 510(k) clearances, and RoHS/REACH material safety compliance.
Medical probes coming into contact with skin or mucosal membranes must pass ISO 10993 cytotoxicity, sensitization, and intracutaneous reactivity testing.
Dual-sourcing of raw materials, automated CNC machining, high-capacity cleanroom assembly lines, and robust buffer stock management to prevent delivery delays.
Tailored thermal sensing architectures designed for diverse clinical, sterilization, and energy recovery applications.
Integrated skin surface temperature sensors, tympanic probes, and esophagus/rectal probe lines compatible with major monitor brands (Mindray, Philips, GE, Nihon Kohden).
High-temperature Pt100 RTD sensor assemblies utilized in horizontal pulse vacuum steam sterilizers and food/beverage shaking retort autoclaves.
Differential temperature and relative humidity sensing nodes for high-efficiency fresh air Energy Recovery Ventilators (ERV) achieving up to 90% heat exchange.
A world-class manufacturer and global supplier committed to advanced, high-quality, and cost-effective healthcare solutions.
Jiangsu Medovia Medical Co., Ltd. is a professional and reliable supplier in the medical equipment industry in China, committed to delivering advanced, high-quality, and cost-effective healthcare solutions to customers worldwide. With years of industry experience and continuous development, we have built a strong reputation as a trusted partner for medical institutions and distributors across the globe.
Our comprehensive product portfolio covers a wide range of medical applications, including surgical equipment, digital and portable X-ray systems, laboratory devices, patient monitors, ECG machines, ultrasound scanners, dental equipment, and hospital furniture. These products are widely used in hospitals, clinics, diagnostic centers, and research laboratories, helping improve efficiency, accuracy, and patient care.
At Jiangsu Medovia Medical, our mission is to provide reliable, innovative, and accessible medical equipment manufactured in China, enabling healthcare providers worldwide to deliver better services.
We strive to:
Our vision is to become a globally recognized brand in the medical equipment industry.
Quality is at the core of everything we do. All our products are manufactured under strict quality control systems and comply with international standards. We are proud that our products are certified by ISO and CE systems, ensuring safety, stability, and performance in clinical environments.
From raw material selection to final inspection, every step of production is carefully monitored to guarantee consistent quality. We also work closely with reputable manufacturers and continuously improve our product line to meet evolving market demands.
Jiangsu Medovia Medical has established an efficient and steadily expanding global marketing and distribution network. Over the years, our products have been exported to more than dozens of countries and regions, including:
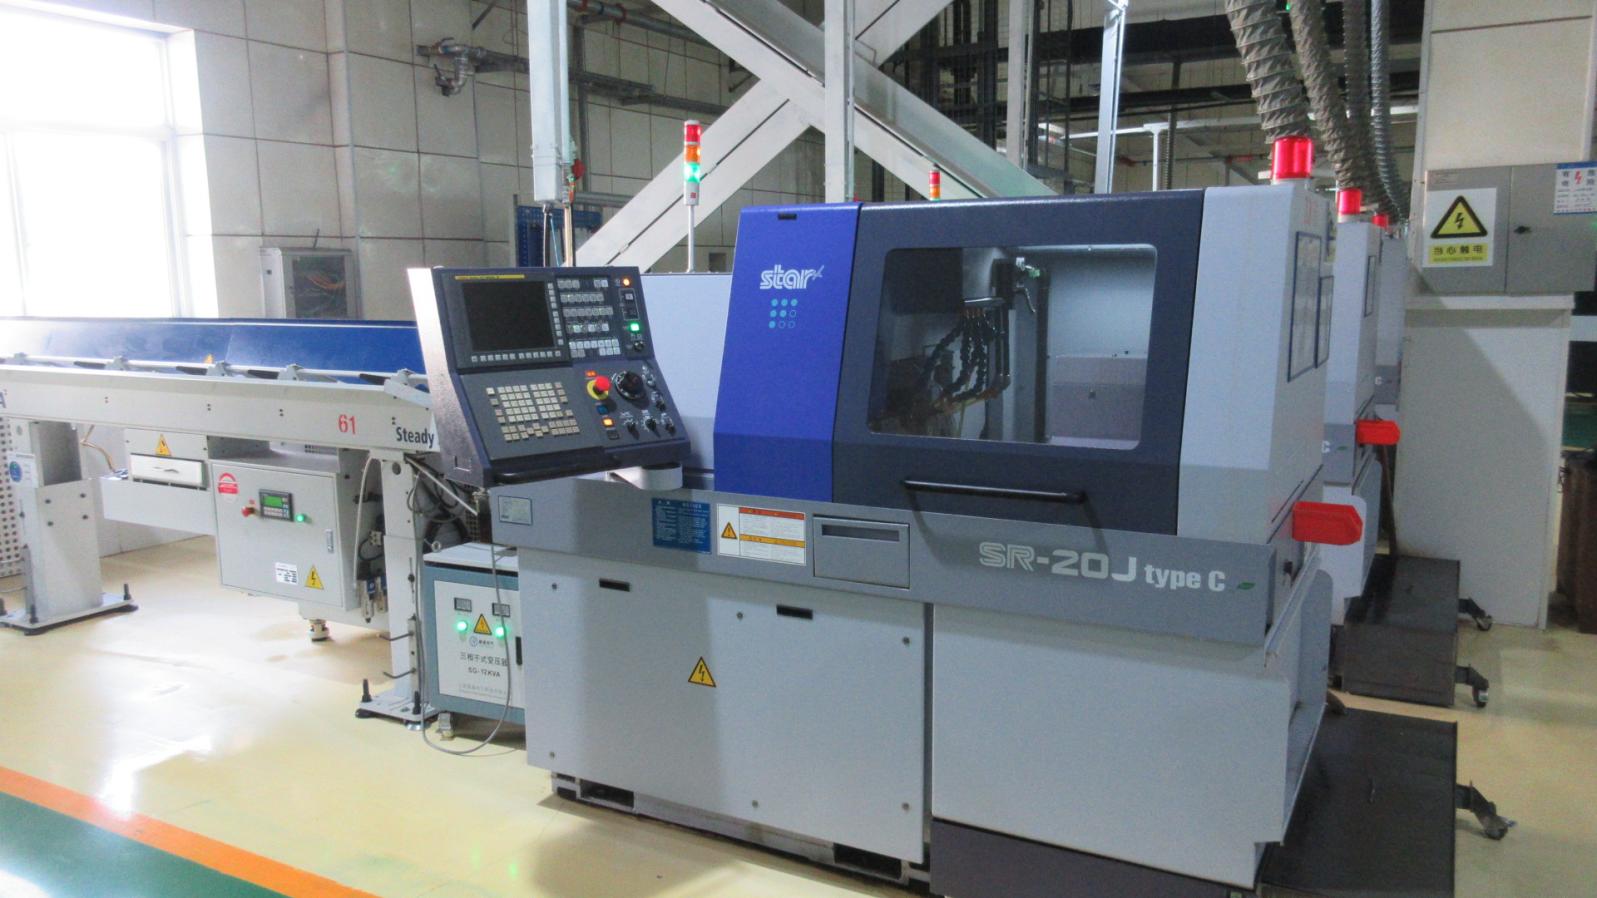
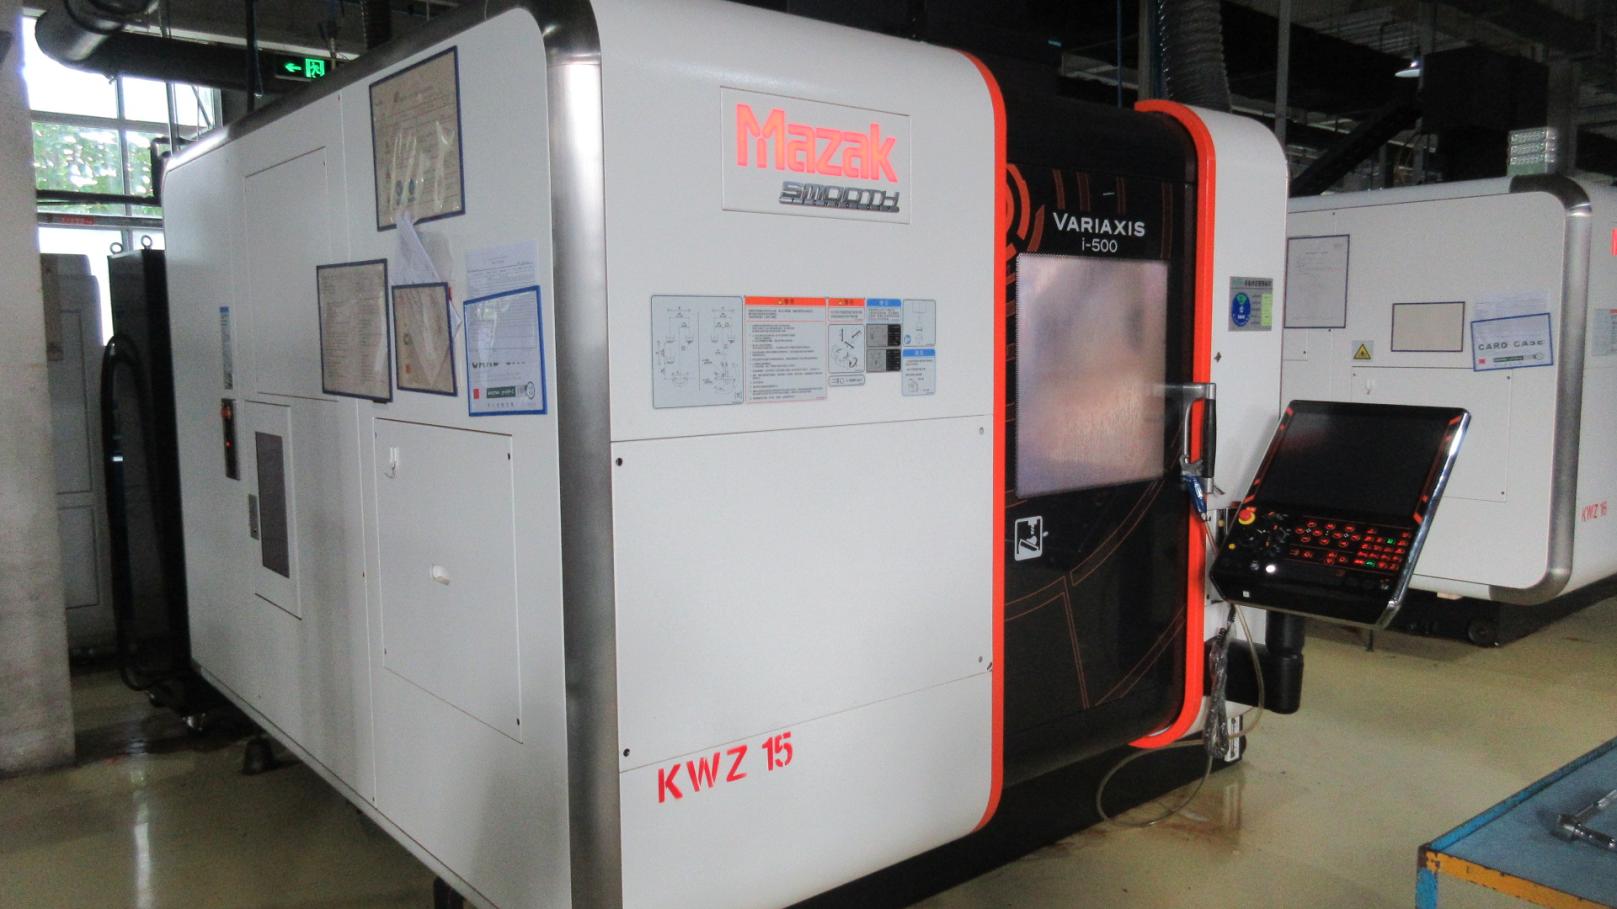
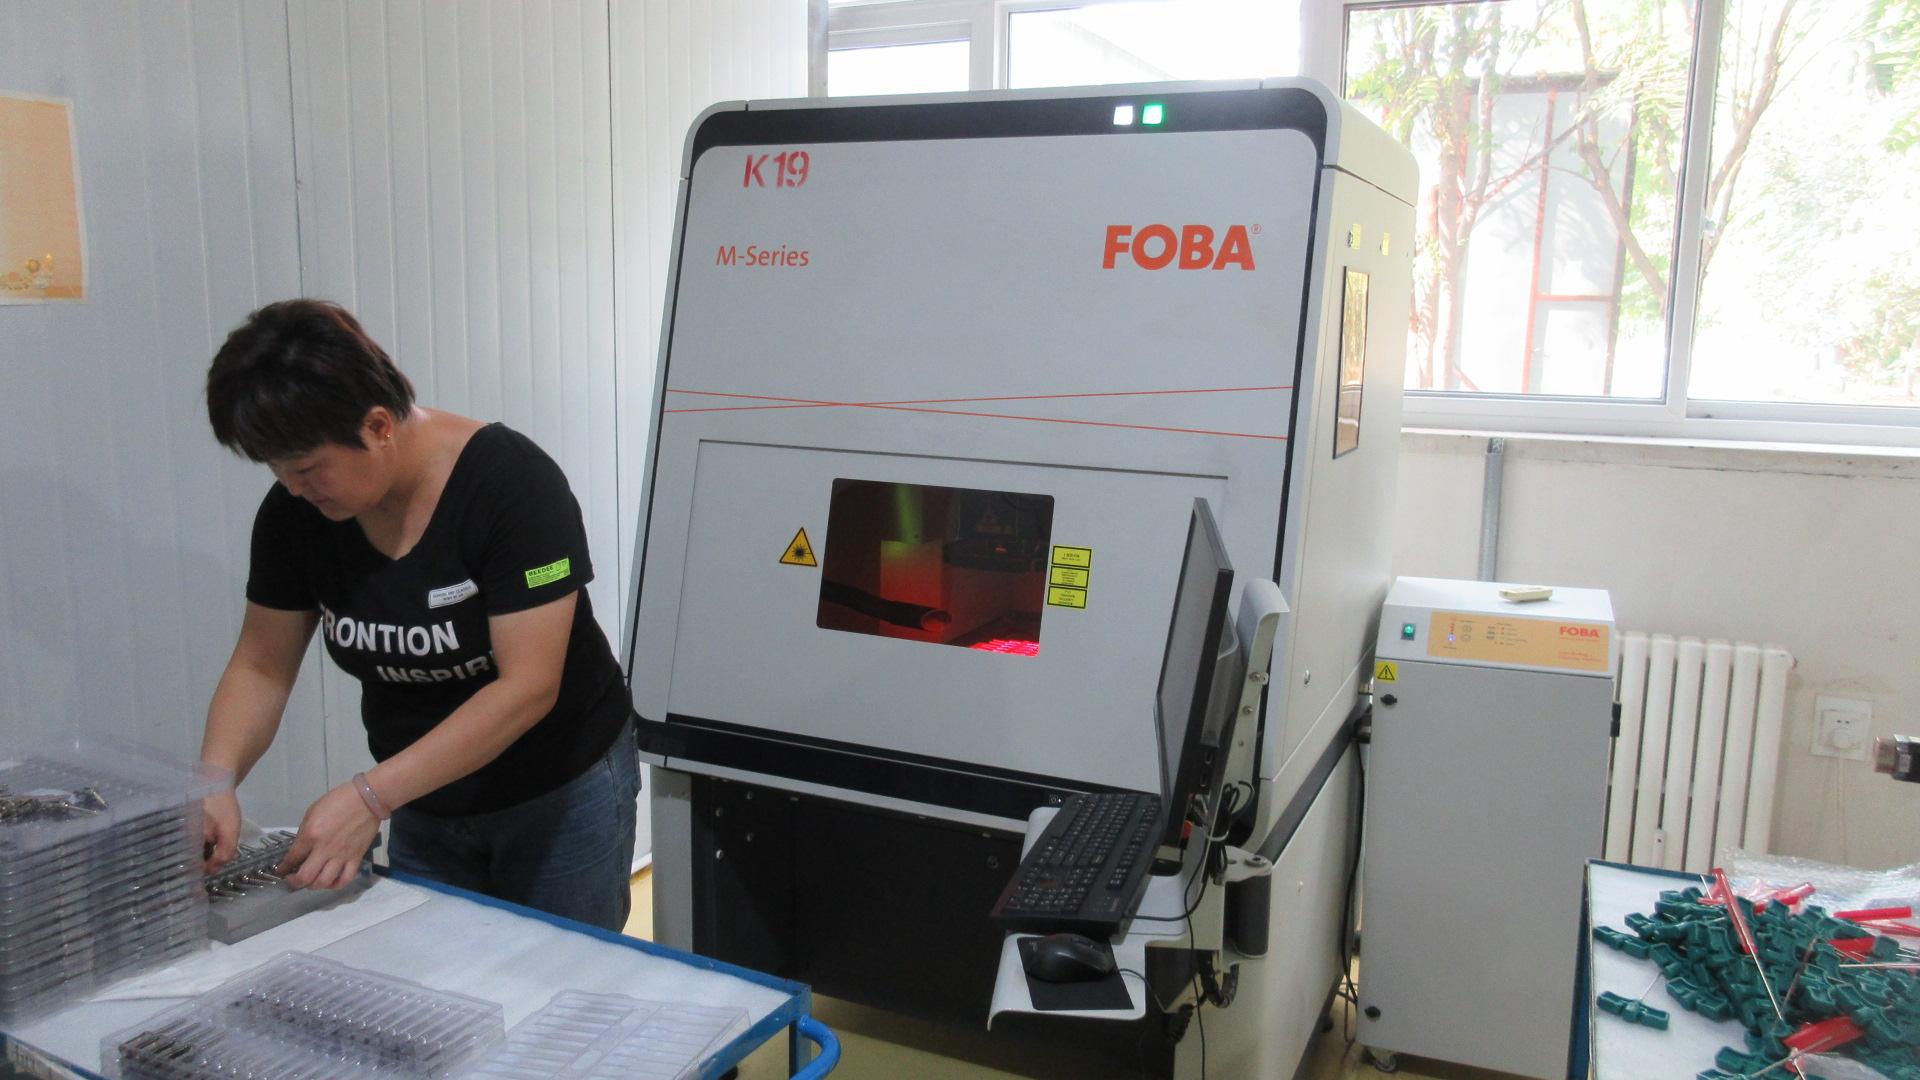
Our state-of-the-art manufacturing infrastructure incorporates multi-axis CNC lathes, high-precision laser engravers, ultrasonic cleaning tanks, and stringent IQC (Incoming Quality Control) inspection stations to deliver uncompromised precision for medical temperature probes and surgical hardware.
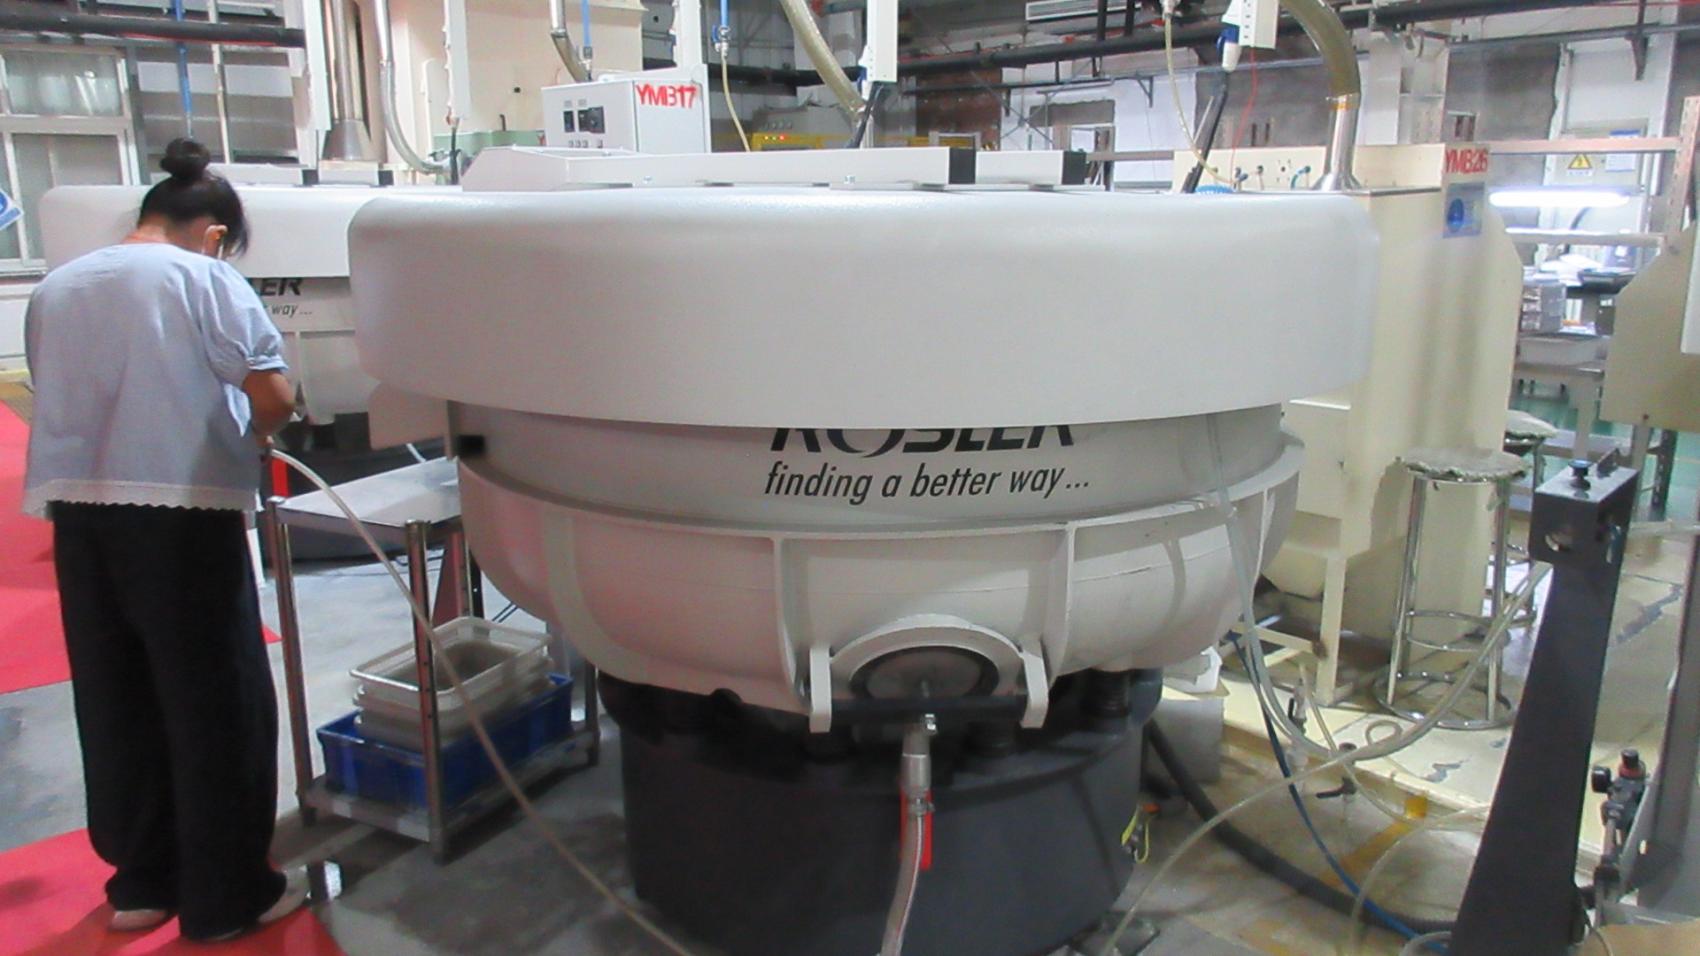
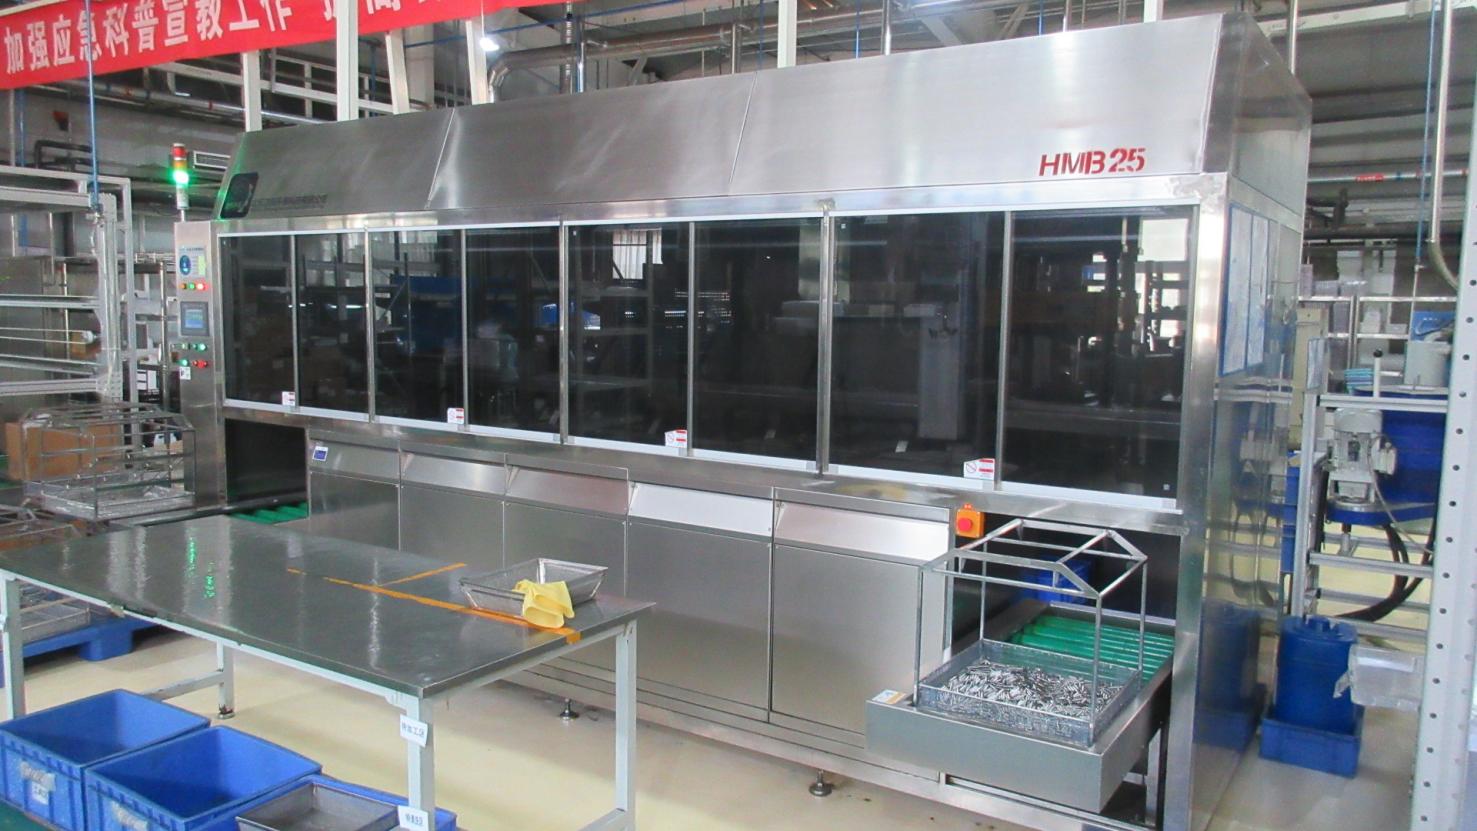
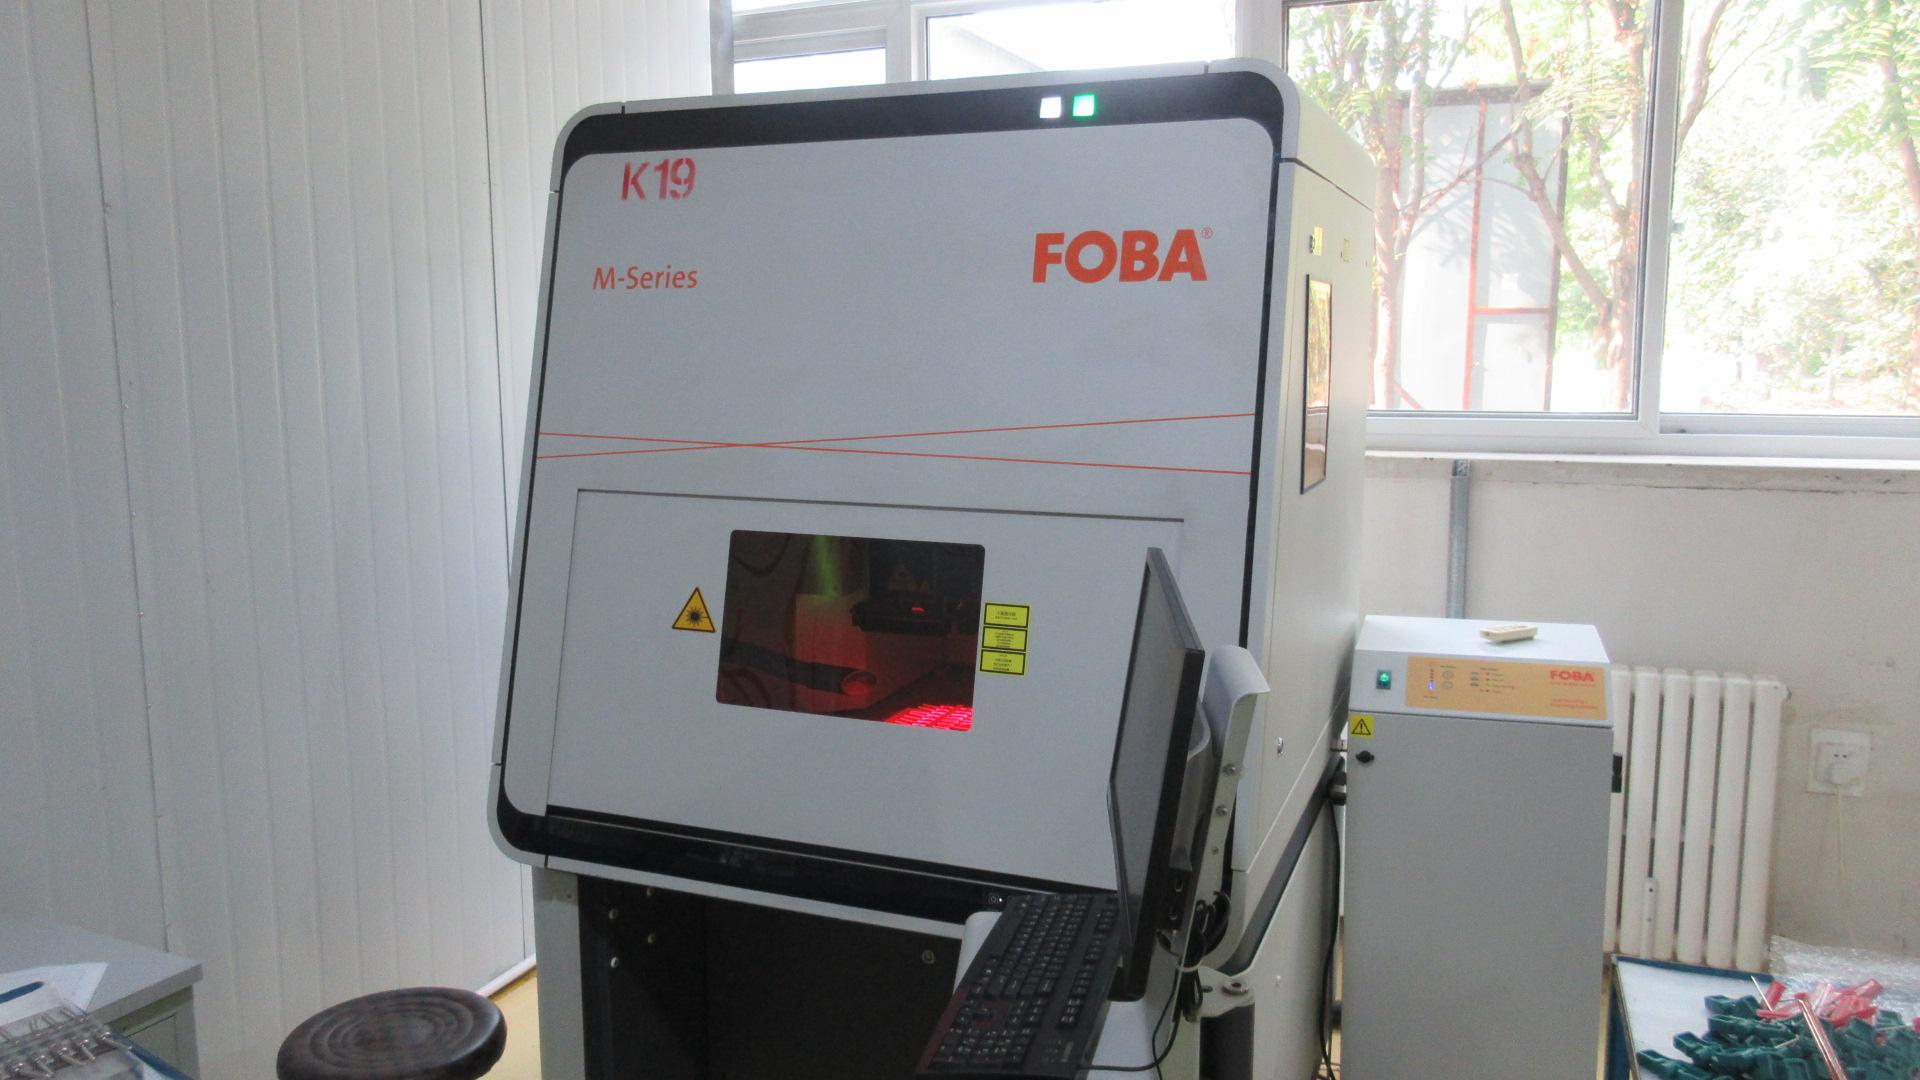
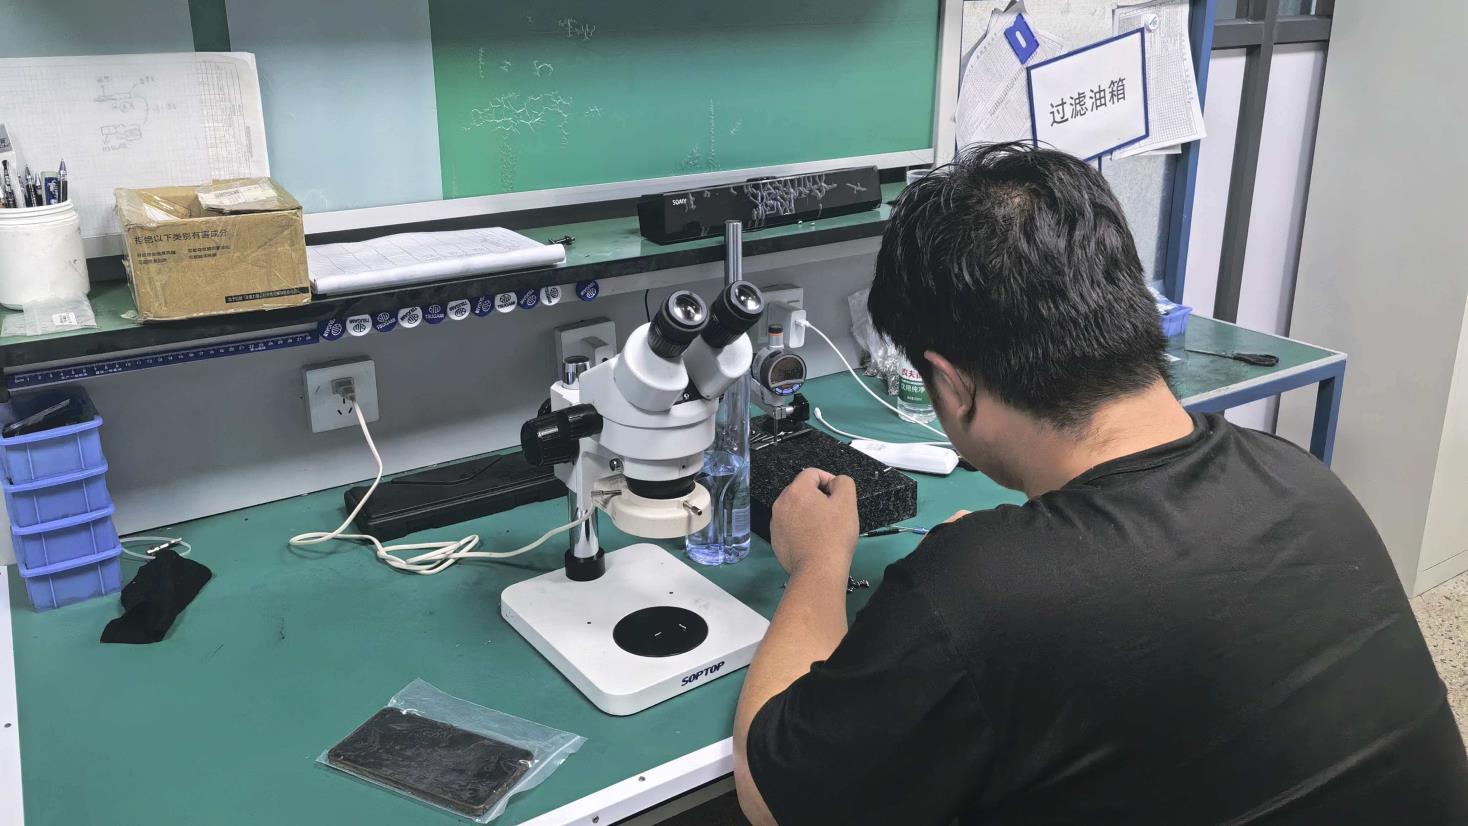
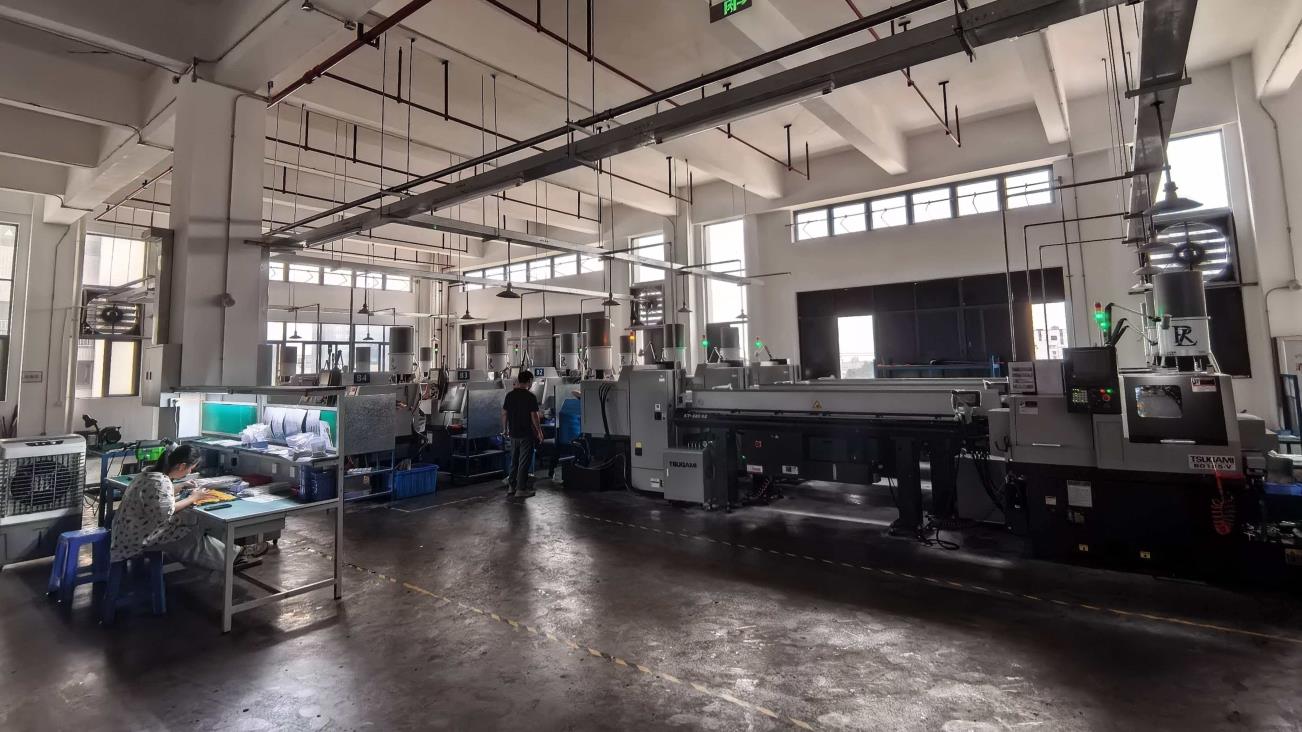
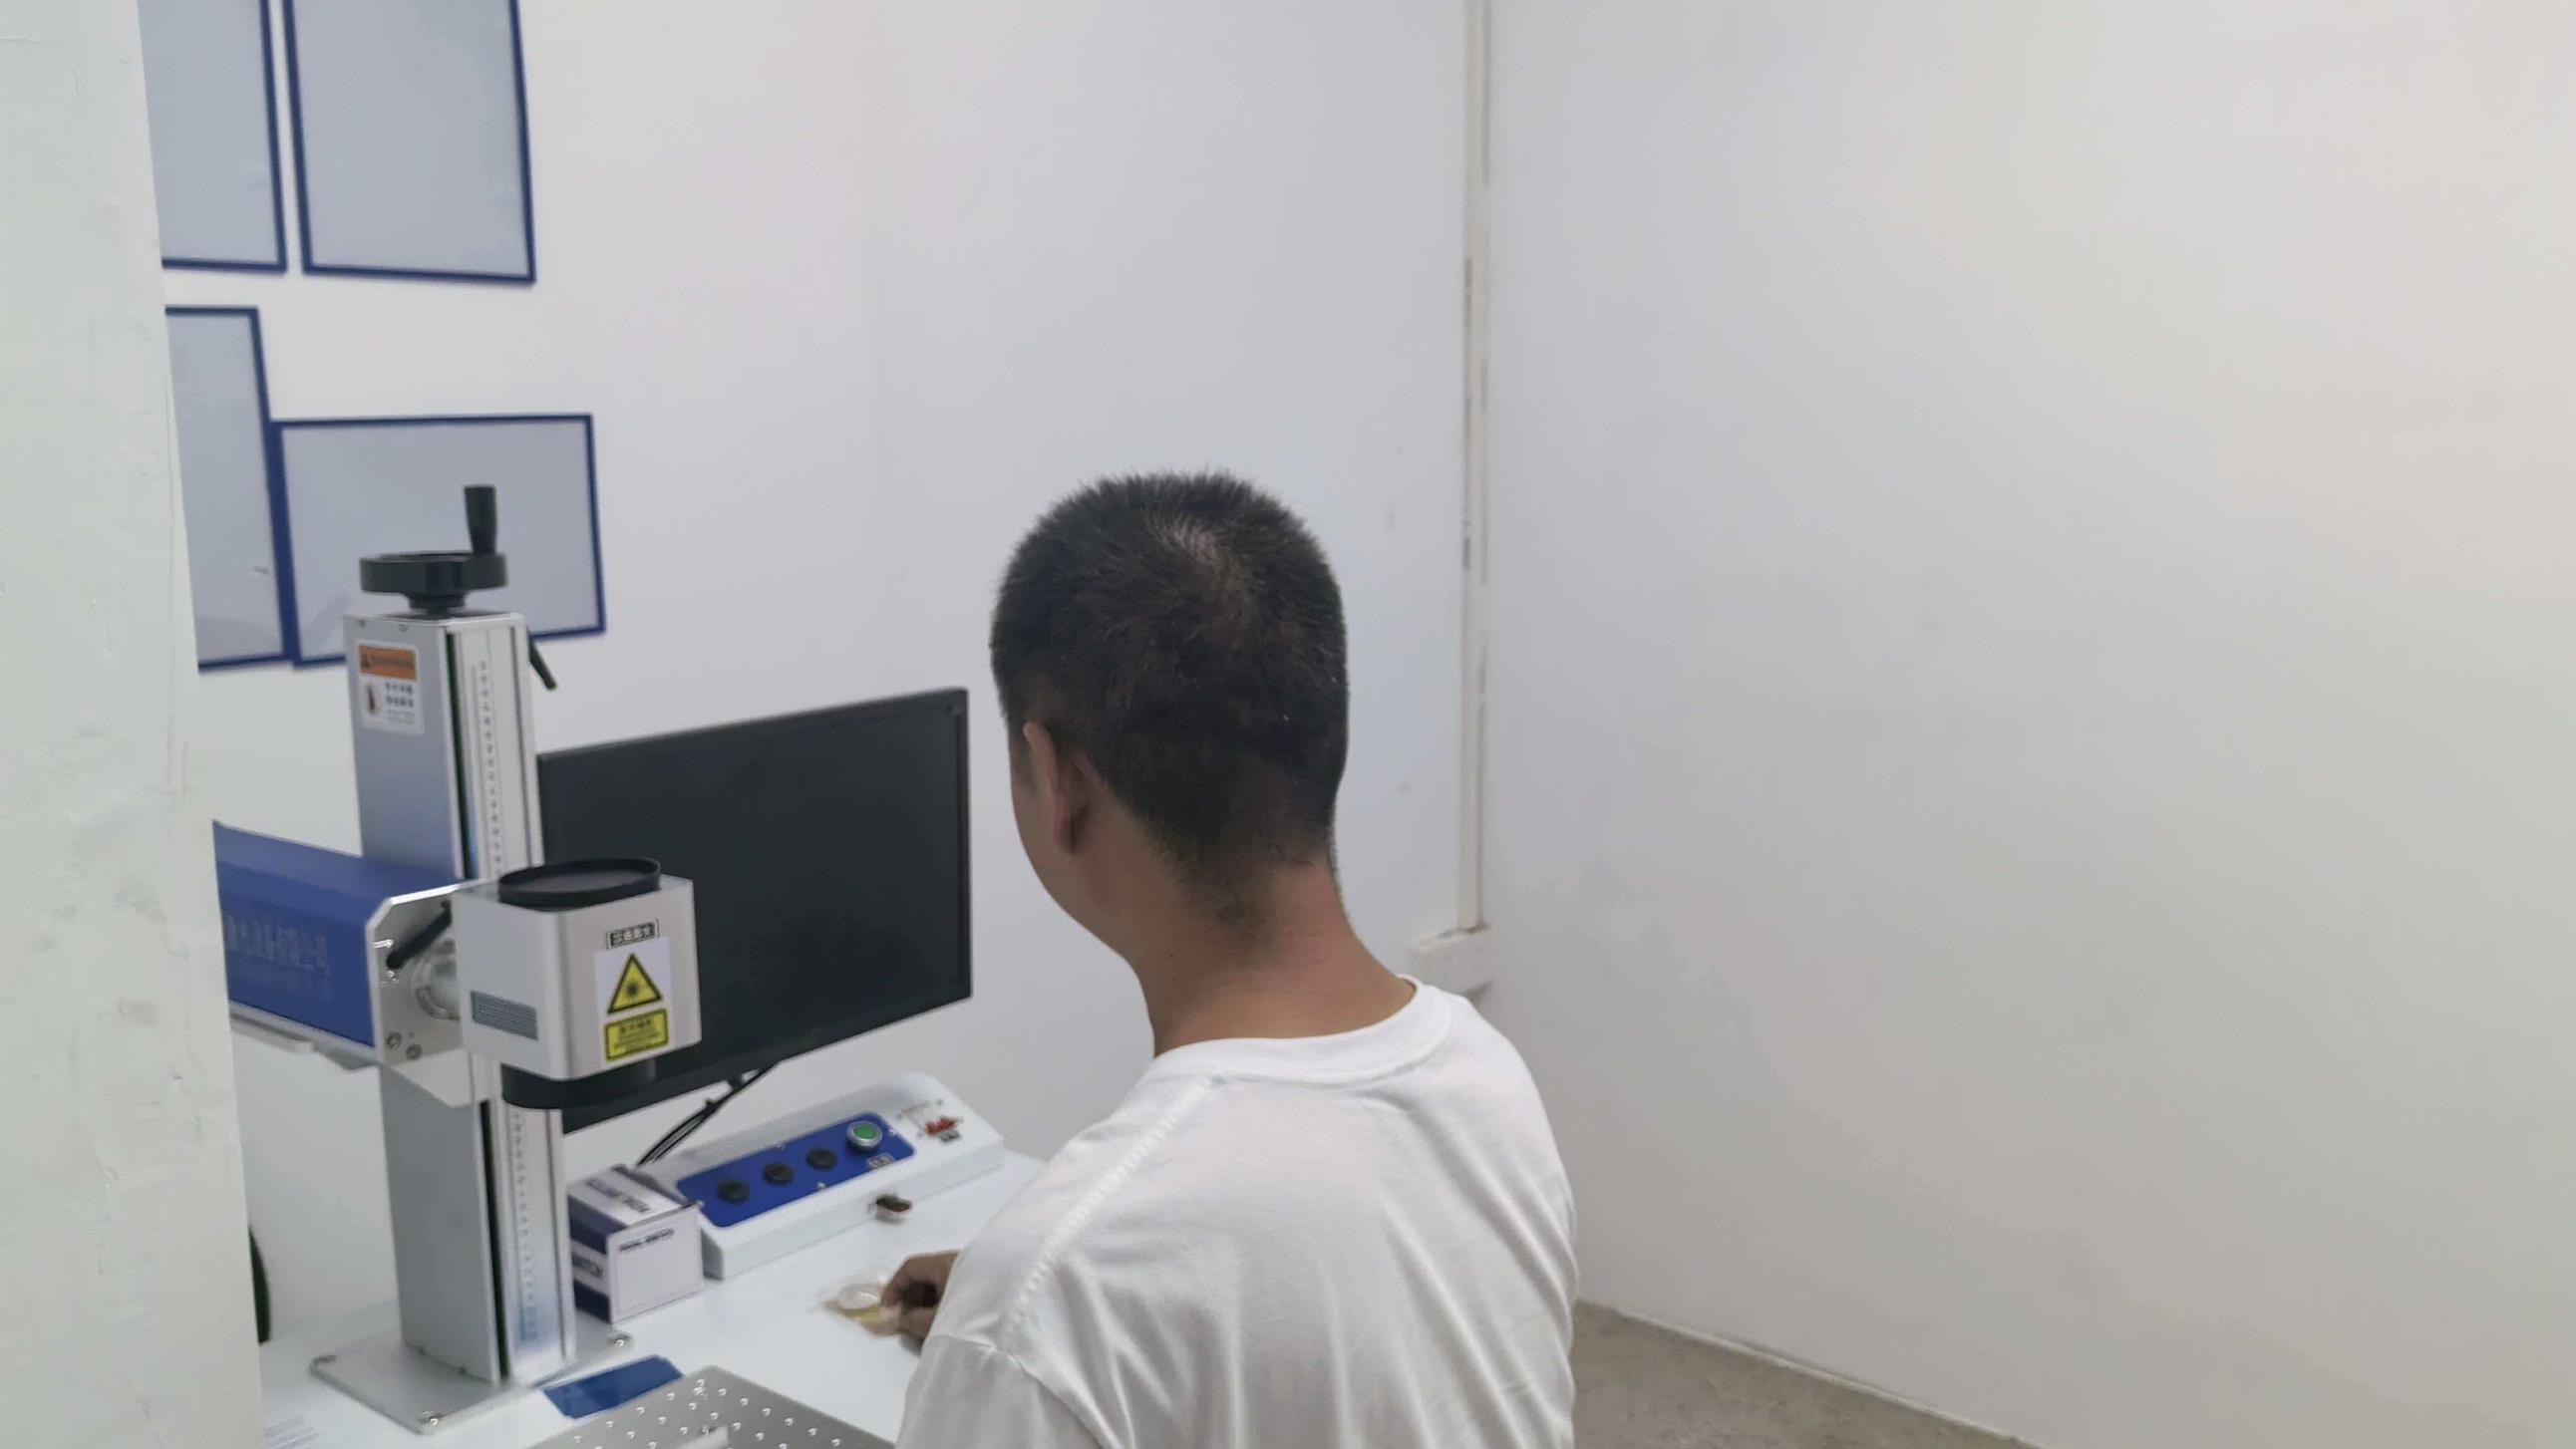
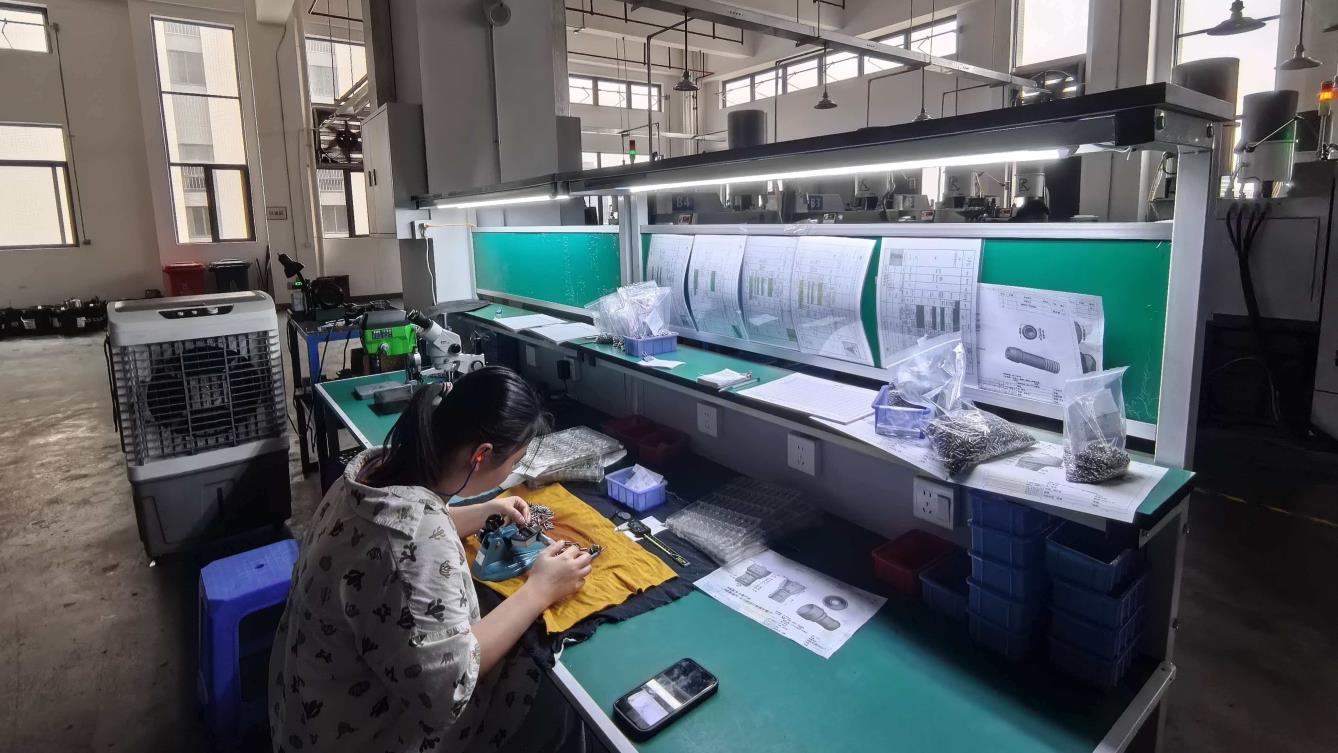
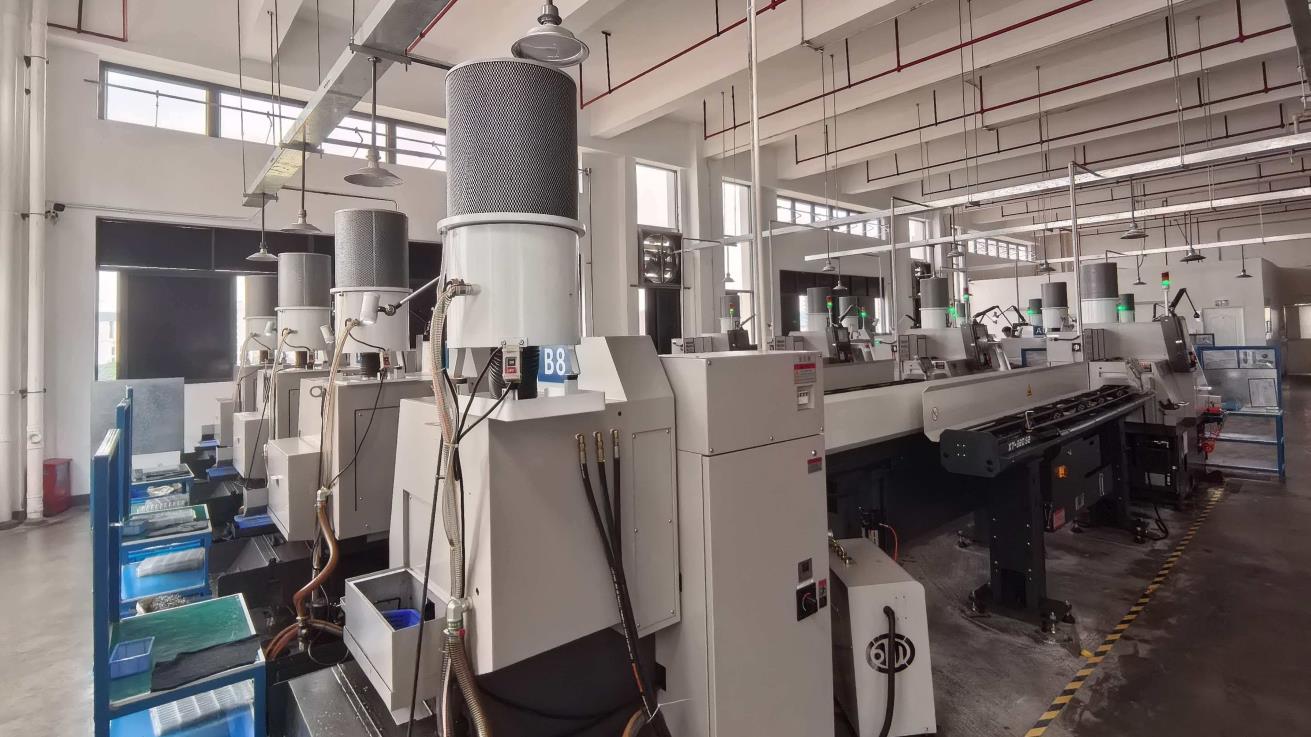
We are dedicated to providing customers with comprehensive one-stop service solutions, making procurement simple, efficient, and worry-free. Our services include:
We sincerely welcome customers from all over the world to visit our manufacturing facilities and explore long-term OEM/ODM cooperation opportunities for a win-win partnership.
Eliminating trade barriers and ensuring seamless regulatory registration in target export markets worldwide.
We assist international distributors with complete Technical Files (STED), Declaration of Conformity (DoC), Certificate of Free Sale (CFS), and ISO 13485 audit reports necessary for local ministry of health registrations.
Localized labeling in English, Spanish, French, Arabic, and Russian. Barcode track-and-trace integration and GS1 UDI (Unique Device Identification) compliant packaging for medical device traceability.
Experienced in FOB, CIF, DDP, and Express Airfreight logistics. Temperature-controlled shipping options available for sensitive calibration devices and electronic hardware.
Pioneering the future of smart thermal diagnostics and connected medical devices.
Transitioning to ultra-thin printed flexible substrate sensors capable of seamlessly conforming to human skin and internal endoscopic instruments without adding bulk.
Embedding micro-reference thermal resistors inside probe cable connectors, enabling self-calibration against internal reference curves upon system power-up.
Developing Fiber Bragg Grating (FBG) optical temperature sensors for high-field MRI environments where metallic thermistors and copper wires are strictly prohibited.
Addressing key technical, quality, and commercial inquiries from global buyers.
Explore our full line of hospital-grade defibrillators, endoscope systems, infusion pumps, and imaging scanners.